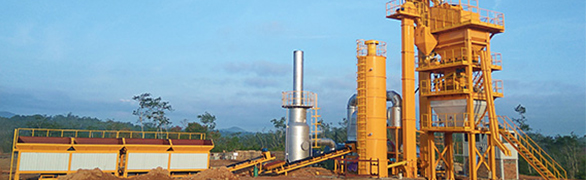
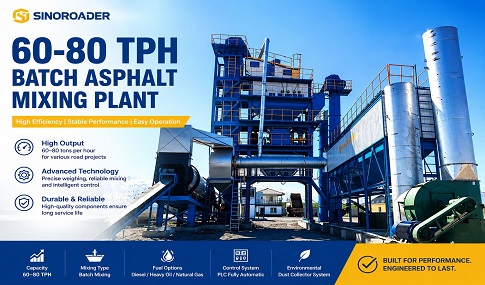
An All-In-One Handbook on Enhancing Asphalt Mixing Plants: Elevating Performance, Minimizing Cost and Maximizing Return on Investment The asphalt mixture plant is the basis of road engineering production. Its operating state has a significant influence on the mixture quality, construction schedule and the enterprise economics benefits. In the process of production, many mixing plants have the problems of lack of the production capacity, high fuel consumption, irregular finished product quality, harsh unplanned standstill, low utilization rate of recycled concrete aggregation. Some enterprises blindly introduce big equipment ignore the by-product optimization of raw materials, process, operation, maintenance, automation details, resulting in huge investment but small returns. Combining the NAPA technical data and the practical production experience, this article systematically elaborates the optimization methods of mixing plant from various aspects, enterprises could make full use of the current existing equipment potential to achieve the goals of higher production capacity, lower energy consumption and higher enterprise profits.
.jpg)
The actual production capacity, energy efficiency, mixture quality stability, and equipment reliability of an asphalt mixing plant are not solely determined by the equipment hardware itself. Rather, they are influenced by a complex interplay of six dimensions: raw material moisture content, production temperature, equipment operating conditions, operation and maintenance management, raw material characteristics, and external conditions of the plant. Many production failures and energy wastes are often caused by the combined effect of multiple factors.
Aggregate drying and heating accounts for 60%-80% of the total energy consumption of a mixing plant, and the moisture content of the aggregates is the primary factor affecting drying energy consumption and production capacity. For every 1% increase in aggregate moisture content, production capacity decreases by 10-12%, fuel consumption increases accordingly, and fine aggregates are more prone to moisture accumulation. More than half of the fuel in the drying drum is used for moisture evaporation, leading to decreased production capacity, increased costs, and defects in the mixed material quality. Enterprises can reduce combustion energy consumption by approximately 21% by lowering the moisture content by methods such as hardening and draining the material yard, providing rain protection for fine aggregates, using dried materials, and installing moisture content sensors. This approach offers low-cost and significant benefits.
The higher the discharge temperature of the asphalt mixture, the lower the production capacity of the mixing plant. For every 1°F increase in the base temperature, the production capacity decreases by 1.5 tons/hour, while energy consumption increases simultaneously. Ambient temperature, wind force, humidity, and altitude also affect production; for every 300 meters increase in altitude, the production capacity decreases by approximately 3.5%. Improper temperature control leads to energy waste and causes asphalt aging, reducing the workability of the mixture. Warm-mix asphalt technology can be used to reduce the production temperature by 30-50°F, saving 8-15% or more in fuel. Under conditions that meet specifications and the dew point of the bag filter, the lowest production temperature should be selected, and parameters should be dynamically adjusted in conjunction with environmental changes.
The structure of the drying drum, the operating condition of the burner, and the status of the bag filter directly determine the heat exchange and output capacity of the mixing plant . A properly commissioned burner can achieve a thermal efficiency of 80-85%, while neglecting maintenance will reduce it to 50-60%. Air leakage in the drum, damage to the lifting plates, and filter bags can also lead to heat loss, reduced production capacity, increased energy consumption, and frequent malfunctions. Meanwhile, metering accuracy, mixing components, pipeline insulation, and frequency converter upgrades also affect production. Enterprises should regularly calibrate the burners, perform preventative maintenance, optimize drum insulation, configure frequency converter drives, and select appropriate lifting plates for the mixed materials.
Frequent start-ups and shutdowns of the mixing plant, exceeding three times per shift, increase fuel consumption by 20-35% compared to continuous steady-state production due to repeated heating losses. Inaccurate metering and proportioning, unreasonable mixing time, overflow of hot material silos, cold start-ups, and neglect of maintenance of components such as bearings, belts, and sensors can all reduce effective production capacity and cause quality defects.
The introduction of PLC and SCADA automated control systems, coupled with online sensors for moisture content and temperature, enables dynamic parameter adjustments, significantly improving production stability. Lack of maintenance and reliance on manual experience-based operation can lead to a series of consequences, including increased downtime, material waste, unstable mix gradation, asphalt content, and inconsistent discharge temperature. In production management, efforts should be made to maintain a stable production rate, effectively utilize finished product storage silos to buffer the supply and demand of transport vehicles, regularly calibrate weighing scales, implement standardized maintenance procedures, and simultaneously provide professional skills training for operators.
Aggregate gradation, dust content, and the proportion of RAP/RAS recycled aggregates significantly alter the operating conditions of a mixing plant. Poor gradation and excessive dust increase the difficulty of asphalt mixing and coating, easily leading to overflow from hot aggregate bins and unstable cold aggregate supply. Increasing the recycled aggregate content requires simultaneous adjustments to the heating logic, with varying impacts on energy consumption and production capacity depending on the equipment used. Simultaneously, the properties of the asphalt binder and admixtures also change the mixing time, coating effect, and required production temperature, especially in intermittent mixing plants, which are prone to quality problems such as non-compliant void ratio and aggregate void ratio (VMA). Enterprises should select stable raw material suppliers, routinely monitor moisture content and gradation, optimize mix proportions, and establish a supporting recycled aggregate processing system to mitigate the adverse effects of raw material fluctuations on production.
Intermittent mixing plants and continuous drum mixing plants have inherently different operating logics. The theoretical capacity listed on the equipment nameplate is calculated under ideal conditions with an aggregate moisture content of approximately 5%. In reality, the actual output on construction sites will almost certainly be lower than the theoretical capacity. Site layout, altitude, and fuel type constitute the basic ceiling for production.
In addition, factors such as the supply of logistics and transportation vehicles, transportation distances, project schedule requirements, and environmental emission and noise control requirements all constrain the actual effective output of a mixing plant. Large-scale mixing plants are more adaptable to high-moisture raw materials and large-volume tasks, but their operating efficiency will significantly decrease when operating at low loads for extended periods.
The core focus of mixing plant optimization is on six key areas: aggregate moisture content control, improved efficiency of the drying and combustion system, optimized mixture temperature, continuous and stable production, full-cycle maintenance, and efficient utilization of recycled materials. Drying and heating consume 60-80% of the overall energy; therefore, the key to cost reduction and efficiency improvement is to reduce the unit energy consumption per ton of mixture while maintaining stable production capacity and mixture quality.
Based on the NAPA QIP-132 technical guideline and extensive factory testing, multiple optimization methods are combined and implemented, resulting in fuel savings of 10-25% or more, increased effective hourly production capacity, reduced downtime, and decreased material waste. The following sections explain the implementable measures in detail.
For every 1% decrease in aggregate moisture content, burner fuel consumption decreases by 10-12%, while effective production capacity increases simultaneously. Moisture evaporation accounts for more than half of the fuel consumption in the drying drum and is the highest priority optimization direction.
Implementation actions:
Expected Benefits: A 1-2 % reduction in aggregate moisture content can result in double-digit percentage fuel savings while increasing hourly production capacity. With hardening of the stockpile yard and rainproofing upgrades, the payback period for most projects can be controlled within one year.
It is recommended that burners undergo professional calibration at least once a year, with the best results achieved before the peak production season. This involves using a flue gas analyzer to calibrate the air-fuel ratio and checking nozzle wear and flame position. Multiple engineering cases show that professional burner calibration can reduce unit energy consumption by 3-11%. Worn nozzles and an unbalanced air-fuel ratio can reduce a burner's thermal efficiency from 80-85% to 50-60%.
Inspect the lifting plates of the drying drum and replace them promptly if wear or deformation is found to ensure sufficient material is lifted and falls, maximizing heat exchange efficiency. While ensuring the safety of the bag filter's dew point, a 10℉ reduction in the exhaust gas temperature at the drum outlet will save approximately 1% of fuel. The temperature difference between the exhaust gas and the mixed material should be controlled within 50℉ as much as possible. Adding an insulation layer to the drying drum can further save 5-10% of energy consumption under certain operating conditions; however, it is essential to refer to the equipment manufacturer's technical specifications before any modifications.
Strictly control excessive combustion air and thoroughly investigate all air leakage points in the cylinder and air duct; install variable frequency drives (VFDs) on high-power motors such as fans and drum drives to adjust the speed according to real-time production load, which saves energy and improves process adjustment capabilities.
By utilizing chemical additives and isothermal mixing technology for asphalt foaming, the discharge temperature of the mixture can be reduced by 30-50℉, resulting in a decrease in fuel consumption of 8-20%. Simultaneously, it reduces asphalt fume emissions and improves the working environment at construction sites. For every 10℉ reduction in production temperature, drying and heating energy consumption decreases by approximately 2-3%.
Subject to project technical specifications, warm-mix technology should be actively adopted, and its effectiveness should be verified through mixture design and on-site testing. If combined with aggregate moisture content control, the energy-saving effects of these two optimizations can be amplified.
Starting and stopping more than 3 times per shift, with repeated heating and cooling, can increase fuel consumption by 20-35%. Production scheduling should be closely coordinated with the on-site paving construction plan, making full use of finished product storage silos to buffer fluctuations in the supply and demand of transport vehicles and reduce frequent downtime caused by material shortages or insufficient vehicles.
Plan for continuous production operations for as long as possible, and avoid short cold starts. Use the number of equipment start-ups and shutdowns per shift as a daily performance indicator (KPI), and simultaneously track fuel consumption per ton of mixed feed to directly assess the losses caused by start-ups and shutdowns.
.jpg)
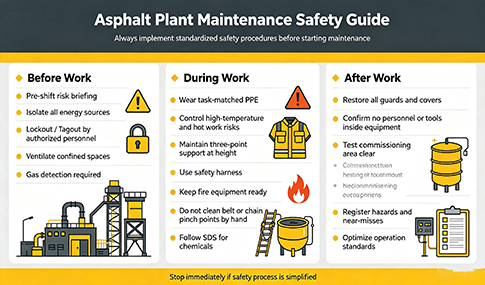
Establish a regular inspection system to promptly replace worn lifting plates, seals, dust filter bags, bearings, conveyor belts, and burner nozzles; calibrate the entire weighing and metering system frequently to prevent waste or substandard materials from leaving the factory due to proportioning deviations.
Insulation was properly applied to all asphalt storage tanks, oil pipelines, flanges, and heat transfer oil pipelines. Leaks in heat transfer oil and steam were repaired immediately. Pipeline insulation upgrades can save considerable fuel costs annually. A stockpile of critical spare parts was established to reduce unplanned downtime caused by sudden failures.
Fully leverage the value of the PLC-SCADA control system to collect real-time data on temperature, fuel consumption, water content, and equipment operating time, shifting from reactive maintenance to predictive maintenance and eliminating faults in their early stages.
When the hardware and mix design of the mixing plant allow, modern mixing plants can generally achieve a recycled material blending ratio of 30-50% or more. Increasing the proportion of recycled material can significantly reduce the procurement costs of new aggregates and new asphalt; for every 10% increase in the proportion of recycled material, raw material costs can be significantly reduced.
To build a system for feeding, metering, and drying recycled materials, we need to ensure accurate metering, reduce waste of asphalt and aggregates by relying on automation, and balance energy consumption and product quality.
Upgrade the PLC/SCADA intelligent control system with moisture content and temperature sensors to achieve automated feeding and one-click recipe recall, reducing human error.
We routinely track key performance indicators (KPIs): energy consumption per ton, hourly production capacity, statistics on downtime failures, stability of discharge temperature , and material loss; we conduct energy benchmarking, referring to public tools such as ENERGY STAR and NAPA to benchmark against industry standards.
Continuously conduct technical training for operators to standardize material handling, temperature parameter settings, and continuous production processes. Optimize the plant's logistics layout to reduce material handling and shorten waiting times for transport vehicles.
Additional other additional instructions to lower costs and improve efficiency If sufficient fuel is available, favor lower-cost clean fuels such as natural gas and determine the viability of electric heating for asphalt storage tank heating. Convert all plant lighting to LED lamps, select motors based on load, and automatically shut down standby auxiliary equipment. Align production schedules with equipment ideal-loads to avoid extended low-load and wasteful operation. Implementation priorities and results expected: Moisture content control, burner calibration, stable continuous production should be given the first priority as they do not require much capital investment and the payback period is short. Then to carry out lifting plate repair, cylinder insulation, warm mixing implementation, frequency converter upgrading and automation upgrading. When the overall optimization is achieved, typically, the unit energy consumption drops 10-20%, the effective production capacity rises, the waste drops down and the maintenance cost drops. The specific result would depends on the condition of the equipment, the mixture type, the climate and the price of fuel. When only the moisture contents control and the production process optimization were carry out, the fuel saving is more than 12%, the saving would be increased when more than one technology were adopted. In order to make measurable improvements to.
The biggest advantage of mobile asphalt mixing plants is their flexibility, enabling them to serve dispersed and sequential road projects. However, mobile mixing plants also have inherent drawbacks: frequent disassembly and relocation, significant differences in aggregate and raw material conditions among various projects, limited site space, and time-consuming disassembly, assembly, and commissioning. Improper handling can severely reduce overall profitability.
The general optimization logic for mixing plants (moisture content control, combustion system, steady-state production, warm mixing and recycled materials) still applies, but needs to be adapted to special scenarios of mobile equipment relocation.
Excessive relocation time is the biggest productivity killer for multi-project operations of mobile stations. Highly modular models, equipped with quick couplings, hydraulic supports, and prefabricated pipelines, can reduce the complete "relocation-commissioning" cycle to 1-3 days; disassembly and assembly of older, non-modular equipment often takes 3-7 days. Industry experience shows that the cost of a single relocation accounts for approximately 3-5% of the equipment value.
Practical points:
Each time a new project is selected, the site foundation, aggregate source, moisture content, and available working space will change.
The site should be flat, well-drained, and close to the stone production area and paving surface. The foundation bearing capacity should be able to support the full load of the silo to avoid foundation settlement.
Material stockpile management remains a top priority. The stockpile base should maintain a 2-4% drainage slope, and the ground should be hardened if conditions permit. Fine aggregates should be equipped with movable rainproof covers, and loaders should prioritize taking the dry material from the top of the stockpile. Even at temporary construction sites, moisture content remains the primary factor determining energy consumption and production capacity; a 1% decrease in moisture content can result in 10-12% fuel savings.
Equipped with a portable moisture content sensor and integrated into the control system, it can quickly adapt to different aggregate raw materials for new projects. Due to site constraints, material supply chain management needs to be more rigorous to ensure stable raw material quality and reasonable feeding sequence.
.jpg)
Adapt the efficient methods of fixed mixing plants to mobile stations: calibrate the burners at least once a year and recheck their operating conditions after major relocations; check the lifting plates and seals for air leaks; configure variable frequency drives for the fan drums as much as possible; and control the exhaust gas temperature appropriately.
Vigorously promote the warm-mix asphalt process, which reduces temperatures by 30-50℉, resulting in 8-20% fuel savings. It also helps cope with ambient temperature fluctuations between projects and is suitable for long-distance transportation of asphalt mixtures. Fully utilize mobile storage silos to buffer transport vehicles, maintain continuous production for extended periods, and avoid the 20-35% additional fuel consumption caused by multiple start-stop cycles per shift.
Most modern mobile mixing plants can incorporate over 30% RAP (Rich Alkali Compound) recycled materials, fully leveraging the cost-reduction advantages of recycled materials. Temporary sites require careful management of recycled material storage to prevent moisture absorption. After each relocation, the weighing system and various sensors must be recalibrated, and the control system must store the mixture formulas for different projects to enable rapid switching and recall between projects.
Mobile mixing plants are ideally suited for integration with PLC/SCADA control systems and remote cloud platform monitoring. They enable basic digitalization through recipe storage, automatic moisture content compensation, and automatic production report generation.
By deploying remote monitoring and IoT-enabled equipment, managers can view energy consumption per ton of material, hourly output, temperature parameters, and equipment runtime from their offices across multiple projects, gaining real-time access to the status of mobile mixing plants at various construction sites. Predictive maintenance is implemented based on sensor data, allowing faults to be resolved during project relocation intervals, avoiding disruption to production windows. A unified control system operating logic reduces the learning curve for operators rotating between projects.
When selecting equipment, do not only look at the peak theoretical capacity. Instead, select equipment based on the normal output of the projects undertaken by the enterprise, and reserve a margin of 15-20% to cope with fluctuations in the moisture content of raw materials and unexpected minor failures. Long-term low-load operation of equipment will significantly reduce economic benefits.
The production rhythm of the mixing plant must be closely coordinated with the paving team and the transportation fleet; a dedicated spare parts warehouse for mobile equipment should be established to ensure the supply of spare parts; and special training should be provided to front-line personnel on relocation and installation, raw material moisture content control, and quality testing.
When conducting project cost estimates, one cannot only look at output; relocation costs, fuel prices at different construction sites, and actual equipment utilization rates must be included in the full life cycle cost accounting.
Performance metrics include: relocation occupancy days , energy consumption per ton of mixture, actual hourly capacity compared to nameplate readings, downtime due to malfunctions, mixture pass rate, and overall production cost per ton of finished product. Modular equipment should be prioritized, operational processes standardized, and emphasis placed on moisture content control and IoT monitoring. Each relocation should be treated as a standardized process rather than a passive production interruption. Continuous optimization should be implemented in conjunction with NAPA QIP-132 technical guidelines for adapting mobile equipment and on-site audits.
KPIs for mixing plants are used to quantitatively evaluate production efficiency, energy consumption, finished product quality, equipment reliability, and production costs. NAPA recommends that it is not necessary to collect massive amounts of data; instead, focus on key indicators. These mainly include six categories: production capacity, energy efficiency, material loss, finished product quality, equipment operation and maintenance, and environmental and financial aspects. They cover key items such as hourly output TPH, capacity utilization rate, energy consumption per ton of mixture, aggregate moisture content, proportion of recycled materials, proportion of waste materials, downtime, and mixture inspection pass rate. Some indicators can also be benchmarked against industry peers using the ENERGY STAR tool to quickly identify production shortcomings.
Implementing KPI management requires establishing a performance baseline by retrieving historical data from the past year and achieving automatic data collection using SCADA and sensors. Weekly anomaly checks and quarterly trend analysis are necessary, combining early warning and outcome indicators for comprehensive judgment. For mobile mixing plants, relocation time statistics also need to be added. Daily monitoring should prioritize core data such as unit energy consumption, capacity utilization rate, recycled material blending, and waste ratio, continuously reviewing and optimizing against NAPA industry benchmarks to drive a steady improvement in mixing plant production efficiency.
Significant efficiency losses at batching plants are not due to equipment hardware defects, but rather to human errors in basic operation, maintenance, and capacity planning. These mistakes consistently lead to high energy consumption, insufficient capacity, fluctuating mix quality, and frequent downtime, eroding return on investment . Based on NAPA industry data, here are some frequently encountered pitfalls:
Moisture content is the primary factor affecting production, yet it is often overlooked by on-site managers. Material piles lack rain protection and drainage slopes; loaders scoop up waterlogged material from the bottom of the piles without monitoring moisture content, and parameters are not adjusted according to changes in raw material moisture. For every 1% increase in moisture content, production capacity drops by 10-12%, while fuel consumption spikes simultaneously.
Mitigation measures: Harden the material pile, implement a 2-4% drainage slope, and cover fine materials for rain protection; prioritize the collection of dry aggregate from the top of the pile; and install a moisture content sensor linked to the burner. Achieving a 1-2% reduction in moisture content can yield considerable energy savings and increased production.
New burners have a thermal efficiency of 80-85%, but this can drop to 50-60% if left uncalibrated for a long time. Worn and detached lifting plates, air leaks in the cylinder duct, air-fuel ratio imbalances, and persistently high exhaust gas temperatures result in a significant waste of heat. Many companies only perform maintenance when equipment completely fails, neglecting regular performance calibration. Mitigation measures include: professionally calibrating burners using a flue gas analyzer before each peak production season; regularly inspecting the lifting plates; sealing air leaks; and controlling exhaust gas temperature within safe dew point limits.
.jpg)
Starting and stopping more than 3 times per shift, with repeated heating and cooling, results in an additional 20-35% in fuel consumption. The root cause is often an unreasonable production plan, insufficient storage capacity, and frequent shutdowns for cleaning the drum due to fluctuations in paving and transport vehicle traffic.
Mitigation measures: Make good use of finished product storage warehouses to buffer supply and demand, match production plans with paving progress, and organize long-term continuous production as much as possible; use the number of start-ups and shutdowns per shift as a daily performance indicator (KPI).
Many companies only look at the peak theoretical output when selecting equipment. However, the equipment operates at low load most of the time, which increases the fixed cost per ton of mixture. The equipment's thermal efficiency decreases in the low load range, resulting in an efficiency loss of about 10%.
Mitigation measures: Select equipment based on normal actual output, reserve a 15-20% margin to cope with raw material fluctuations, and prioritize ensuring that the equipment operates in the most efficient load range, rather than blindly pursuing large nameplate capacity.
Worn conveyor components, malfunctioning baghouse dust collectors, and inaccurate metering systems, if not addressed promptly, gradually lead to sudden shutdowns and quality defects. Industry statistics show that 80% of sudden shutdowns stem from a lack of routine inspections and maintenance. Forgetting to recalibrate the weighing sensors after relocation is an even more frequent cause of errors at mobile mixing plants.
Mitigation measures: Establish preventative maintenance plans during off-seasons and production gaps; stockpile critical spare parts; conduct mandatory calibration of the weighing scales after each relocation of a mobile station; and shift towards predictive maintenance based on operational data.
Production parameters were not corrected for changes in moisture content; the weighing equipment was not calibrated for a long time, and the mixing equipment was worn out, resulting in poor gradation and asphalt coating effects; multiple parameters were modified at once during commissioning, making it impossible to pinpoint the root cause when problems occurred; and the equipment was not recalibrated after relocation or component replacement.
Mitigation measures: Regularly calibrate the metering system; adjust only one parameter at a time, observe the results, and then continue; if possible, introduce warm mixing technology to lower the target production temperature; and correct the drying conditions by matching the measured moisture content in real time.
The ground where the material was piled was not hardened, resulting in poor drainage; aggregates of different specifications were mixed together; recycled RAP material was simply and haphazardly piled up, becoming damp and clumping, and was treated as a secondary material. This caused material segregation, contamination, large production fluctuations, and increased waste.
Mitigation measures: Optimize the material flow line in the material yard; manage recycled materials to the same standards as new aggregates, and ensure rain protection and screening; reduce the risk of moisture segregation caused by secondary material handling.
Relying entirely on the experience of veteran workers to judge the production status, lacking systematic indicator recording, leads to high energy consumption, declining production capacity, and increased waste. It is only after costs have risen sharply that people realize the problem.
Mitigation measures: Focus on tracking energy consumption per ton, capacity utilization rate, recycled material efficiency, waste ratio, and causes of failure; compare with NAPA industry theoretical benchmarks; and achieve visual monitoring through automated systems.
.jpg)
A properly maintained main steel structure of a mixing plant can serve for 20-30 years, but core subsystems such as burners, control systems, and drying drums have a lifespan of only 10-15 years, requiring regular assessments of the necessity for upgrades. When issues arise such as continuously rising energy consumption, frequent equipment failures leading to increased downtime, fluctuating mix quality that fails to meet specifications, mismatch between production capacity and business operations, inability to adapt to new environmental regulations, or severely outdated technology, it is necessary to consider upgrading or replacing the equipment. Do not wait until the equipment is completely paralyzed before taking reactive measures; instead, assess the equipment status promptly by comparing it against various decision-making thresholds and considering actual production conditions.
Regarding equipment upgrade decisions, if the main structure of the mixing plant is intact, and only some subsystems have shortcomings, partial upgrades should be prioritized, as this approach requires lower investment and yields a faster return on investment. However, if multiple core components age simultaneously, and upgrades cannot address the shortcomings in production capacity, environmental protection, and recycled material processing, resulting in high maintenance and inefficient operating costs, then complete plant replacement should be considered. Overall decision-making should not be based solely on subjective experience; it requires collecting KPI operating data, calculating economic benefits, and conducting energy audits and financial calculations before making a final judgment.
Standardized mixing plants, with their generic design, are difficult to adapt to a company's raw materials, production capacity, site conditions, and environmental requirements. Customized mixing plants, on the other hand, can be tailored to specific needs, including production capacity layout, drying and combustion systems, automation platforms, recycled material modules, warm mixing processes, mobile modular structures, and wear-resistant components. This addresses the drawbacks of a "one-size-fits-all" approach, effectively reducing energy consumption, increasing production capacity, minimizing material loss, and stabilizing the quality of the final mixed product. In some scenarios, it can even lead to significant savings in fuel and raw material costs.
Customized upgrades can bring a 5-20% increase in production efficiency and a 10-25% reduction in fuel consumption, but the hardware advantages need to be matched with material yard management, stable production, and KPI management to be realized. Enterprises should first analyze their own production data to identify bottlenecks, prioritize the upgrading of high-return modules, select equipment manufacturers that can perform engineering customization, and simultaneously implement personnel training and spare parts support to fully realize the value of customized equipment and obtain better long-term investment returns.
Achieving cost reduction, increased production, and improved quality in asphalt mixing plants does not solely rely on purchasing new, large-scale equipment. Numerous enterprise practices have shown that implementing fundamental measures such as aggregate moisture content control, combustion drying system maintenance, stable and continuous production, standardized maintenance, and KPI data management can yield significant benefits. After basic optimization is completed, component modifications, automation, and customized upgrades can then be considered. For mobile mixing plants, careful management of disassembly and relocation is crucial to minimize relocation losses. Regardless of whether the plant is fixed or mobile, optimization results must be validated using production data and evaluated in conjunction with ROI assessments. Only by establishing a closed loop encompassing raw materials, operation and maintenance, digitalization, and investment calculation can the full potential of equipment be unleashed, helping enterprises build a competitive advantage in a cost-fluctuating market.